
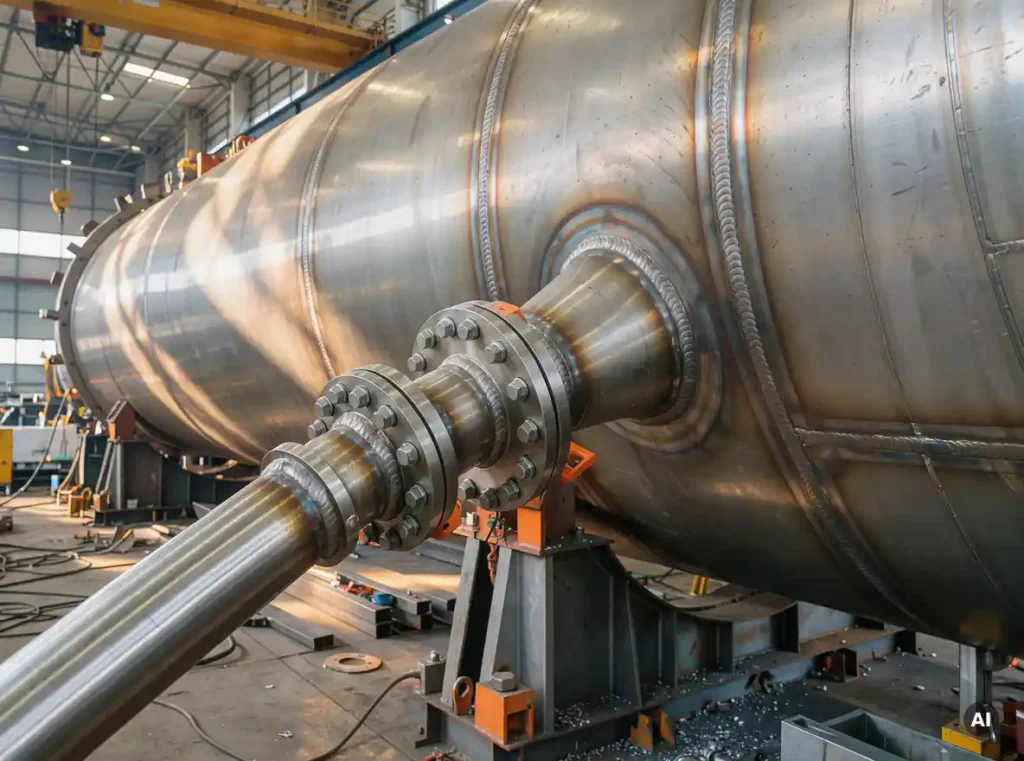
Why does oxygen mass transfer limit autoclave performance?
Oxygen mass transfer limits autoclave performance because oxidation reactions can only proceed as fast as dissolved oxygen reaches the mineral surface. Oxygen has low solubility in hot, acidic slurry, so the rate at which gas dissolves often becomes the bottleneck for sulfide oxidation. In refractory gold pressure oxidation, sulfide minerals such as pyrite and arsenopyrite must be broken down to release the gold locked inside them. That reaction consumes large volumes of oxygen. If gas transfer into the liquid lags behind demand, oxidation stalls, residence time must increase and recovery suffers. Several factors govern the transfer rate:- Bubble size: smaller bubbles expose more gas surface area per unit volume.
- Agitation intensity: stronger shear breaks gas into finer bubbles and renews the liquid film around them.
- Oxygen partial pressure: higher partial pressure raises the driving force for dissolution.
- Slurry properties: density, viscosity, temperature and solids content all change how readily oxygen dissolves.
Where is oxygen injected inside a multi-compartment autoclave?
Oxygen is injected into each agitated compartment of a multi-compartment autoclave, typically below the impeller or close to its discharge zone. Placing the gas where shear is highest ensures it breaks into small bubbles immediately and spreads through the slurry rather than rising straight to the vapor space. A horizontal pressure oxidation autoclave is divided by internal baffles, called weirs, into several compartments. Slurry flows from one compartment to the next, and each compartment has its own agitator. Oxygen demand is not equal across compartments. The first compartments usually see the most intense oxidation, because the freshest, most reactive sulfides are present there. For that reason, oxygen supply is commonly split and controlled per compartment. Operators can then send more gas where the reaction is strongest and trim flow where demand has fallen. Individual flow control also helps maintain the target oxygen partial pressure in the vapor space of each compartment. The injection point matters as much as the flow rate. Gas released in a poorly agitated zone tends to coalesce into large bubbles that escape quickly, wasting oxygen.What equipment delivers and disperses oxygen in the slurry?
Oxygen is delivered through sparge pipes or lances connected to an external gas supply, then dispersed by the compartment agitator. The lance carries gas into the vessel and releases it near the impeller, while the agitator turns that gas into a fine bubble cloud mixed throughout the slurry. The delivery chain generally follows this sequence:- High-purity oxygen is supplied from an on-site plant or storage system.
- A control and metering system regulates pressure and flow for each compartment.
- Oxygen travels through piping and enters the autoclave through dedicated nozzles.
- Internal sparge pipes or lances route the gas to the injection point beneath or beside the agitator.
- The agitator impeller shears the gas into small bubbles and circulates them through the slurry.
Which materials withstand oxygen sparging in acidic autoclaves?
Titanium is the standard material for oxygen sparging components and autoclave linings in acidic pressure oxidation service. It forms a stable oxide layer that resists hot, acidic, chloride-bearing slurry, which is why titanium-clad autoclaves are widely used for both gold pressure oxidation and nickel and cobalt leaching. Autoclave shells are usually built in carbon steel for strength, with a corrosion-resistant lining on the process side. Titanium grades such as Grade 17 have been used for autoclave linings, and design details have evolved over the years to address erosion, one of the most common field problems. Brick and lead linings protect carbon steel in other designs, but the titanium cladding approach keeps the structural wall slim and simplifies the construction. Erosion deserves as much attention as corrosion. Injection points, lance tips and areas close to the agitator experience high local velocities and abrasive solids. Designers address this through:- careful selection of titanium grades for internals and cladding
- local thickness allowances or protection at high-wear points
- smooth internal geometry that avoids turbulence-inducing crevices
What safety risks come with high-pressure oxygen in autoclaves?
The main safety risk is oxygen enrichment, which makes materials ignite more easily and burn far more intensely than in air. In an autoclave, high-pressure oxygen in contact with hydrocarbons, fine metal particles or contaminated surfaces can start a fire that is extremely difficult to control. The principal hazards include:- Ignition of contaminants: oils, greases and organic residues can ignite in pure oxygen, so oxygen service demands rigorous cleaning.
- Metal combustion: some metals, including titanium under certain conditions, can burn in oxygen-rich environments if mechanically damaged or exposed to particle impact.
- Pressure and temperature excursions: exothermic oxidation reactions can accelerate if oxygen supply exceeds demand.
- Gas velocity effects: high flow velocities in oxygen piping can generate friction and particle impact that become ignition sources.
How is oxygen delivery designed for large autoclaves?
Oxygen delivery for large autoclaves is designed by matching oxygen demand to compartment layout, agitator capacity and vessel geometry. The goal is to supply enough oxygen at the right location with adequate dispersion, while keeping internals mechanically sound across a very large vessel. The design typically builds on process requirements supplied by the technology owner or EPC contractor. These define the oxidation duty, operating pressure, temperature and slurry characteristics. The mechanical design then has to turn those inputs into a vessel that delivers them reliably. Key design considerations include:- Compartment sizing and weir layout: these shape slurry flow and residence time in each oxidation stage.
- Agitator selection: power, impeller type and shaft arrangement must support gas dispersion across the full compartment.
- Nozzle and lance positioning: openings must be reinforced and located to avoid stress concentrations while placing gas where it is needed.
- Thermal and structural loads: large vessels expand, carry heavy internal loads and require well-designed supports.
- Fabrication and transport: very large autoclaves weigh several hundred tons, so manufacturability and logistics influence the design from the outset.
How Coek helps with oxygen delivery in pressure oxidation autoclaves
Coek engineers and fabricates custom industrial autoclaves for demanding pressure oxidation and acid leaching duties. Process requirements come from the customer, EPC contractor or technology owner, and Coek translates them into mechanically sound, manufacturable equipment. Coek’s relevant capabilities include:- Titanium-clad autoclave construction, including Ti Grade 17 lining experience and design refinements to address erosion
- Large-scale fabrication, with autoclave references approaching 1,000 tons
- Mechanical engineering of nozzles, internals and support structures with fabrication efficiency in mind
- Compliance with international standards, including ISO 9001, PED and ASME
- Integrated equipment scope where appropriate, covering related mechanical systems and components
Frequently Asked Questions
How do I know if my autoclave is oxygen-limited rather than limited by reaction kinetics?
A common sign is that sulfide oxidation improves when you raise agitator speed, increase oxygen flow or raise vapor-space oxygen partial pressure, without changing temperature or residence time. If these changes have little effect, the reaction itself or slurry chemistry is more likely the constraint. Tracking oxygen consumption, off-gas composition and sulfide oxidation per compartment helps separate the two cases.
What are the first steps in specifying an oxygen delivery system for a new pressure oxidation autoclave?
Start with the process data from your technology owner or EPC contractor: oxidation duty, operating pressure, temperature, slurry density and expected oxygen demand per compartment. From there, define the number of compartments, agitator duty, number and position of lances, and the oxygen supply and metering scheme. Involving the autoclave fabricator early lets you check nozzle layout, titanium internals and manufacturability before the design is frozen.
What should I do if oxygen utilization is low and a lot of oxygen is leaving with the off-gas?
First check the dispersion: confirm that the lance outlet sits in the high-shear zone near the impeller, that the agitator is running at its design speed and power, and that the lance is not damaged or blocked. Then review whether oxygen flow per compartment matches demand, since oversupplying a compartment with low demand wastes gas. Excess solids, viscosity changes or foaming can also hurt gas dispersion, so check slurry properties as well.
What are the most common causes of lance or sparger failure in service?
Erosion from abrasive slurry near the lance tip and agitator is the most frequent cause, followed by vibration-related fatigue from inadequate support and blockage by scale or solids. Good mounting, smooth geometry, appropriate titanium grades and local wear protection reduce these risks. Regular inspection during planned shutdowns lets you catch thinning or cracking before it leads to an unplanned outage.
How should oxygen piping be cleaned and maintained to stay safe?
Oxygen piping and components should be cleaned to a recognized oxygen service standard to remove oils, greases and particles before commissioning. After any maintenance that opens the system, repeat the cleaning and inspection and keep contaminants such as lubricants and organic residues out of the work area. Combined with limits on gas velocity, compatible materials and protective interlocks, this significantly lowers the ignition risk.
Can I increase autoclave throughput just by raising oxygen flow?
Not usually. Extra oxygen only helps if it dissolves into the slurry, which depends on bubble size, agitator capacity and partial pressure. Beyond a point, additional gas escapes to the vapor space and can push up pressure and reaction heat. Debottlenecking typically needs a review of agitator power, injection locations, cooling capacity and off-gas handling together, not oxygen flow alone.
How do design codes like PED and ASME affect oxygen injection nozzles and internals?
These codes govern wall thickness, nozzle reinforcement, inspection and testing, all of which apply to the penetrations that carry oxygen lances into the vessel. Nozzle size and position must keep stress concentrations within code limits, which can constrain where lances can be placed. Considering the code requirements together with process needs at the start avoids costly redesign later.
Related Articles
- How does the filled weight of a mining autoclave affect its support requirements?
- What are the main fabrication challenges of large industrial process columns?
- Why do some industrial processes require custom-built pressure vessels?
- What materials are used to manufacture pressure vessels?
- How do you select the right pressure vessel for your process?